read the article
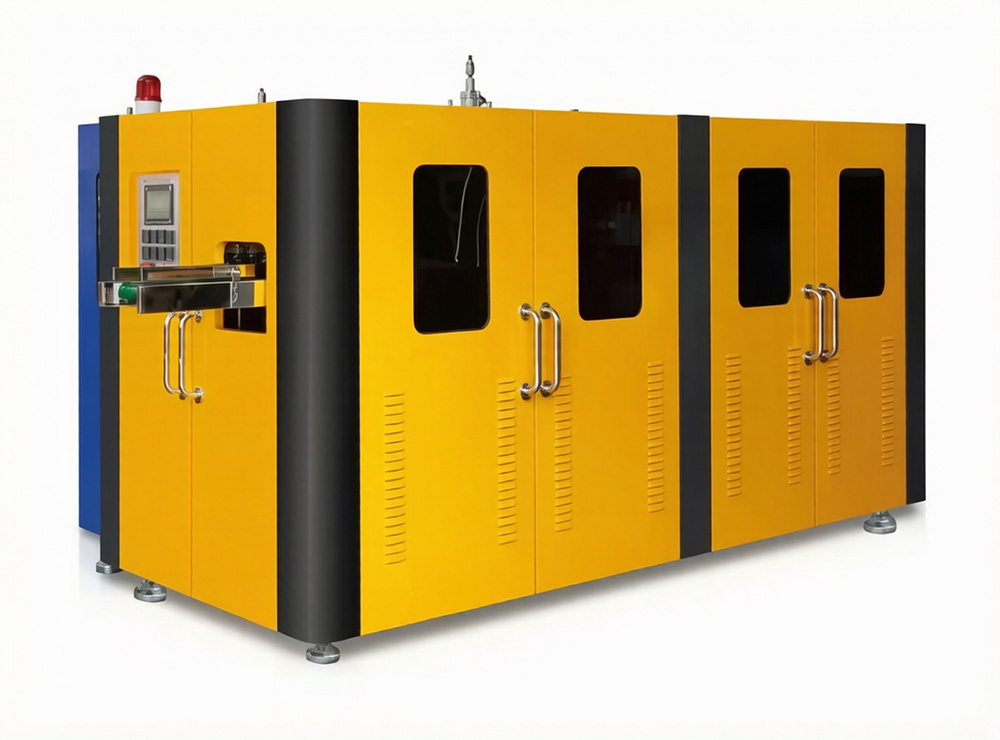
In high-volume bottled water and beverage packaging, hitting a sustained output of 12,600 bottles per hour (BPH) on a 9-cavity fully automatic PET stretch blow molding line requires tight coordination between cavitation geometry, cycle time optimization, and mechanical uptime. Yet high-speed commodity lines face a persistent operational dilemma: maximizing hourly throughput on a single container format often penalizes flexibility when plants must switch between SKUs—such as 350ml, 500ml, or 1.5L bottles—across tight production schedules.
As a specialized Chinese manufacturer of PET stretch blow molding machines and turnkey blowing solutions, tztaixiang engineered a 9-cavity fully automatic system equipped with servo-assisted mold change to deliver 12,600 BPH while drastically cutting SKU changeover downtime. This technical case study examines the kinematics, thermal control, and rapid-changeover architecture behind this high-output installation.
1. The Operational Challenge: High-Speed Output vs. Changeover Downtime
A regional beverage and water manufacturer operating multi-shift bottling lines sought to scale capacity to 12,600 BPH without sacrificing the agility needed for seasonal promotions and multi-SKU retail distribution. Auditing their existing setup revealed four key bottlenecks:
- Cycle Time Ceiling on Multi-Cavity Formats: Reaching 12,600 BPH across 9 cavities requires completing a full molding cycle in approximately 2.57 seconds per index/cycle equivalent, leaving zero margin for sluggish stretch-rod motion, uneven preform heating, or slow mold locking.
- Extended Mold Changeover Stoppages: Manual bolt-unfastening, heavy lifting alignment, and re-shimming across multi-cavity mold halves often consumed 2.5 to 4 hours per changeover, eroding weekly line availability.
- Thermal & Pneumatic Drift at High Speed: Running at rapid cycling rates can cause preform surface-to-core temperature gradients or pressure drops in high-pressure air manifolds if heating zones and valve timing are not tightly synchronized.
- High Utility Intensity per Bottle: Continuous high-speed operation amplifies electricity and compressed-air costs unless heating efficiency and air-recycling features are built into the line architecture.
2. Engineering Solutions by tztaixiang
To sustain 12,600 BPH and streamline SKU transitions, tztaixiang combined high-speed 9-cavity blowing kinematics with precision servo mold change engineering:
A. 9-Cavity Pitch & High-Speed Cycle Optimization
tztaixiang configures 9-cavity platforms with optimized cavity pitch and compact mechanical travel to maximize output per square meter of floor space. Precision-guided stretch rods, responsive pre-blow and high-blow valve sequencing, and balanced infrared heating zones allow preforms to reach target stretch temperatures cleanly and expand uniformly within tight cycle windows.
B. Servo-Driven Mold Change & Repeatable Alignment
Traditional mold swaps rely heavily on manual wrenching and trial-and-error alignment. With tztaixiang’s servo mold change system, automated clamping/locking actuators and servo-controlled positioning/indexing mechanisms guide mold carriers smoothly along precision linear rails with repeatable reference stops—reducing mechanical setup time and minimizing post-changeover tuning scrap.
C. Multi-Zone Heating, Air Recovery & Stable Discharge
To protect bottle clarity, base centering, and wall thickness at 12,600 BPH, the line integrates zoned infrared lamp control, filtered high-pressure air delivery with air-recovery options, and smooth servo-synchronized bottle take-out and discharge conveyors that prevent tipping or scuffing at high speeds.
3. Performance Benchmarks: Conventional Setup vs. tztaixiang 9-Cavity Servo Line
The table below highlights the operational improvements achieved with the tztaixiang 9-cavity fully automatic line featuring servo mold change:
| Performance & Operational Metric | Conventional Multi-Cavity Setup | tztaixiang 9-Cavity Servo Line |
|---|---|---|
| Target Production Output | 7,500 – 9,500 BPH | 12,600 BPH (Continuous Automatic Operation) |
| Cavity Configuration | 6 – 8 Cavities | 9 Cavities (Space-Optimized High-Speed Pitch) |
| Mold Changeover Execution | Manual fastening & prolonged alignment | Servo-assisted mold change & repeatable positioning |
| Process & Discharge Stability | Higher sensitivity to thermal/air lag at speed | Synchronized heating, blowing & smooth discharge |
4. Conclusion: Turnkey PET Blow Molding Expertise from tztaixiang
Achieving 12,600 BPH on a 9-cavity fully automatic line with servo mold change demonstrates how high-speed output and rapid SKU flexibility can work together when mechanical kinematics, thermal profiles, and changeover automation are engineered as a unified system.
As a specialized Chinese manufacturer of PET stretch blow molding machines and turnkey blowing solutions, tztaixiang supports beverage, water, edible oil, and packaging producers with custom cavity configurations, preform-to-bottle process matching, and dependable equipment engineering. Contact the tztaixiang engineering team today to evaluate your target BPH, mold changeover requirements, and complete production line layout.